Stainless steel is iron alloyed with at least 10.5% chromium — and that chromium is the whole trick. It reacts with oxygen to form an invisible, self-repairing oxide film across the surface that stops rust before it starts. Everything else about the metal, from the grades you specify to the price you pay, follows from that one piece of chemistry.
This guide covers what stainless steel actually is, what goes into it, how it’s made from scrap to finished product, and how the two grades you’ll encounter most — 304 and 316 — differ in ways that matter when you’re specifying material.
What is stainless steel?
Stainless steel isn’t a single material. It’s a family of iron-based alloys that share one defining requirement: a minimum of 10.5% chromium by mass. Below that threshold the metal behaves like ordinary carbon steel and rusts. At or above it, something different happens.


What makes stainless steel “stainless”
Chromium at the surface reacts with oxygen in air or water to form a layer of chromium oxide only a few nanometres thick — far too thin to see. This passive layer is dense, chemically stable, and tightly bonded to the metal beneath, so oxygen and moisture can’t reach the iron underneath and turn it to rust.
Add nickel and the crystal structure changes, making the alloy tougher and easier to form and weld. Add molybdenum and the passive layer becomes far more resistant to chlorides. Those two additions are essentially the difference between the grades you’ll be choosing between.
What is stainless steel made of?
Every stainless grade is a deliberate balance of elements, each doing a specific job:
| Element | Typical range | What it does |
|---|---|---|
| Iron | Balance | Base metal — provides strength and structure |
| Chromium | 10.5–26% | Forms the passive oxide layer; the defining element |
| Nickel | 0–22% | Stabilises the austenitic structure; adds ductility, toughness and weldability |
| Molybdenum | 0–7% | Sharply improves resistance to chlorides and pitting |
| Carbon | ≤0.08% (≤0.03% in L grades) | Adds hardness, but must stay low to avoid carbide precipitation |
| Manganese | ≤2% | Deoxidises during melting; can partly substitute for nickel |
| Nitrogen | Trace–0.5% | Boosts strength and pitting resistance, notably in duplex grades |
| Silicon, phosphorus, sulphur | Trace | Residuals from processing, held to tight limits |
Carbon deserves a note, because it explains a designation you’ll see constantly. Between roughly 425°C and 870°C, carbon bonds with chromium at the grain boundaries and forms chromium carbides — pulling chromium out of the surrounding metal and leaving those zones with too little to maintain the passive layer. The result, called sensitisation, shows up as corrosion along weld heat-affected zones. Low-carbon “L” grades like 304L and 316L cap carbon at 0.03% specifically to prevent it, which is why they’re specified for welded assemblies.
How is stainless steel made?
Modern stainless production is a continuous chain from recycled scrap to finished mill product. Most stainless steel made today is 60–70% recycled material — the alloying elements survive remelting indefinitely, so scrap is a feedstock rather than a waste stream.
Melting in an electric arc furnace
Stainless scrap, ferrochrome, nickel and other ferroalloys are charged into an EAF, where graphite electrodes strike an arc and melt the charge at roughly 1,500–1,600°C. A single heat typically runs 60–100 tonnes and takes several hours. The heat number assigned here follows the material through every later step — it’s what makes mill certification traceable.
Decarburisation (AOD)
The molten metal transfers to an argon oxygen decarburisation vessel. Oxygen burns out excess carbon, while injected argon dilutes the carbon monoxide produced — which shifts the chemistry so carbon oxidises preferentially instead of the chromium. Without this step, removing carbon would strip out the expensive chromium along with it. AOD is why stainless became affordable at scale.
Final alloy adjustment
With carbon at target, the exact chemistry is trimmed — chromium, nickel, molybdenum and nitrogen adjusted to land inside the specified range for the grade being produced. Samples are analysed and corrected before the heat is released. This is the point where a heat becomes 304, 316L or a duplex grade.
Casting
The liquid steel is continuously cast into semi-finished shapes: slabs for flat products, blooms and billets for long products and seamless pipe. The strand solidifies as it’s withdrawn and is cut to length.
Hot rolling
Reheated to around 1,100–1,300°C, slabs pass through rolling stands that reduce them to plate or hot-rolled coil. Billets are rolled to bar, or pierced and elongated over a mandrel to produce seamless tube and pipe.
Annealing and pickling
Hot work leaves the metal stressed and covered in oxide scale. Solution annealing — heating to roughly 1,010–1,120°C then quenching rapidly — dissolves carbides back into solution and restores full corrosion resistance. Pickling in acid then strips the scale and re-passivates the surface.
Cold rolling and finishing
Where thinner gauges, tighter tolerances or specific surfaces are needed, material is cold rolled, re-annealed and finished — producing the 2B, No. 4 and BA finishes specified for sheet. Products are then cut, tested and certified against the applicable standard before shipping.
How pipe and tube are made
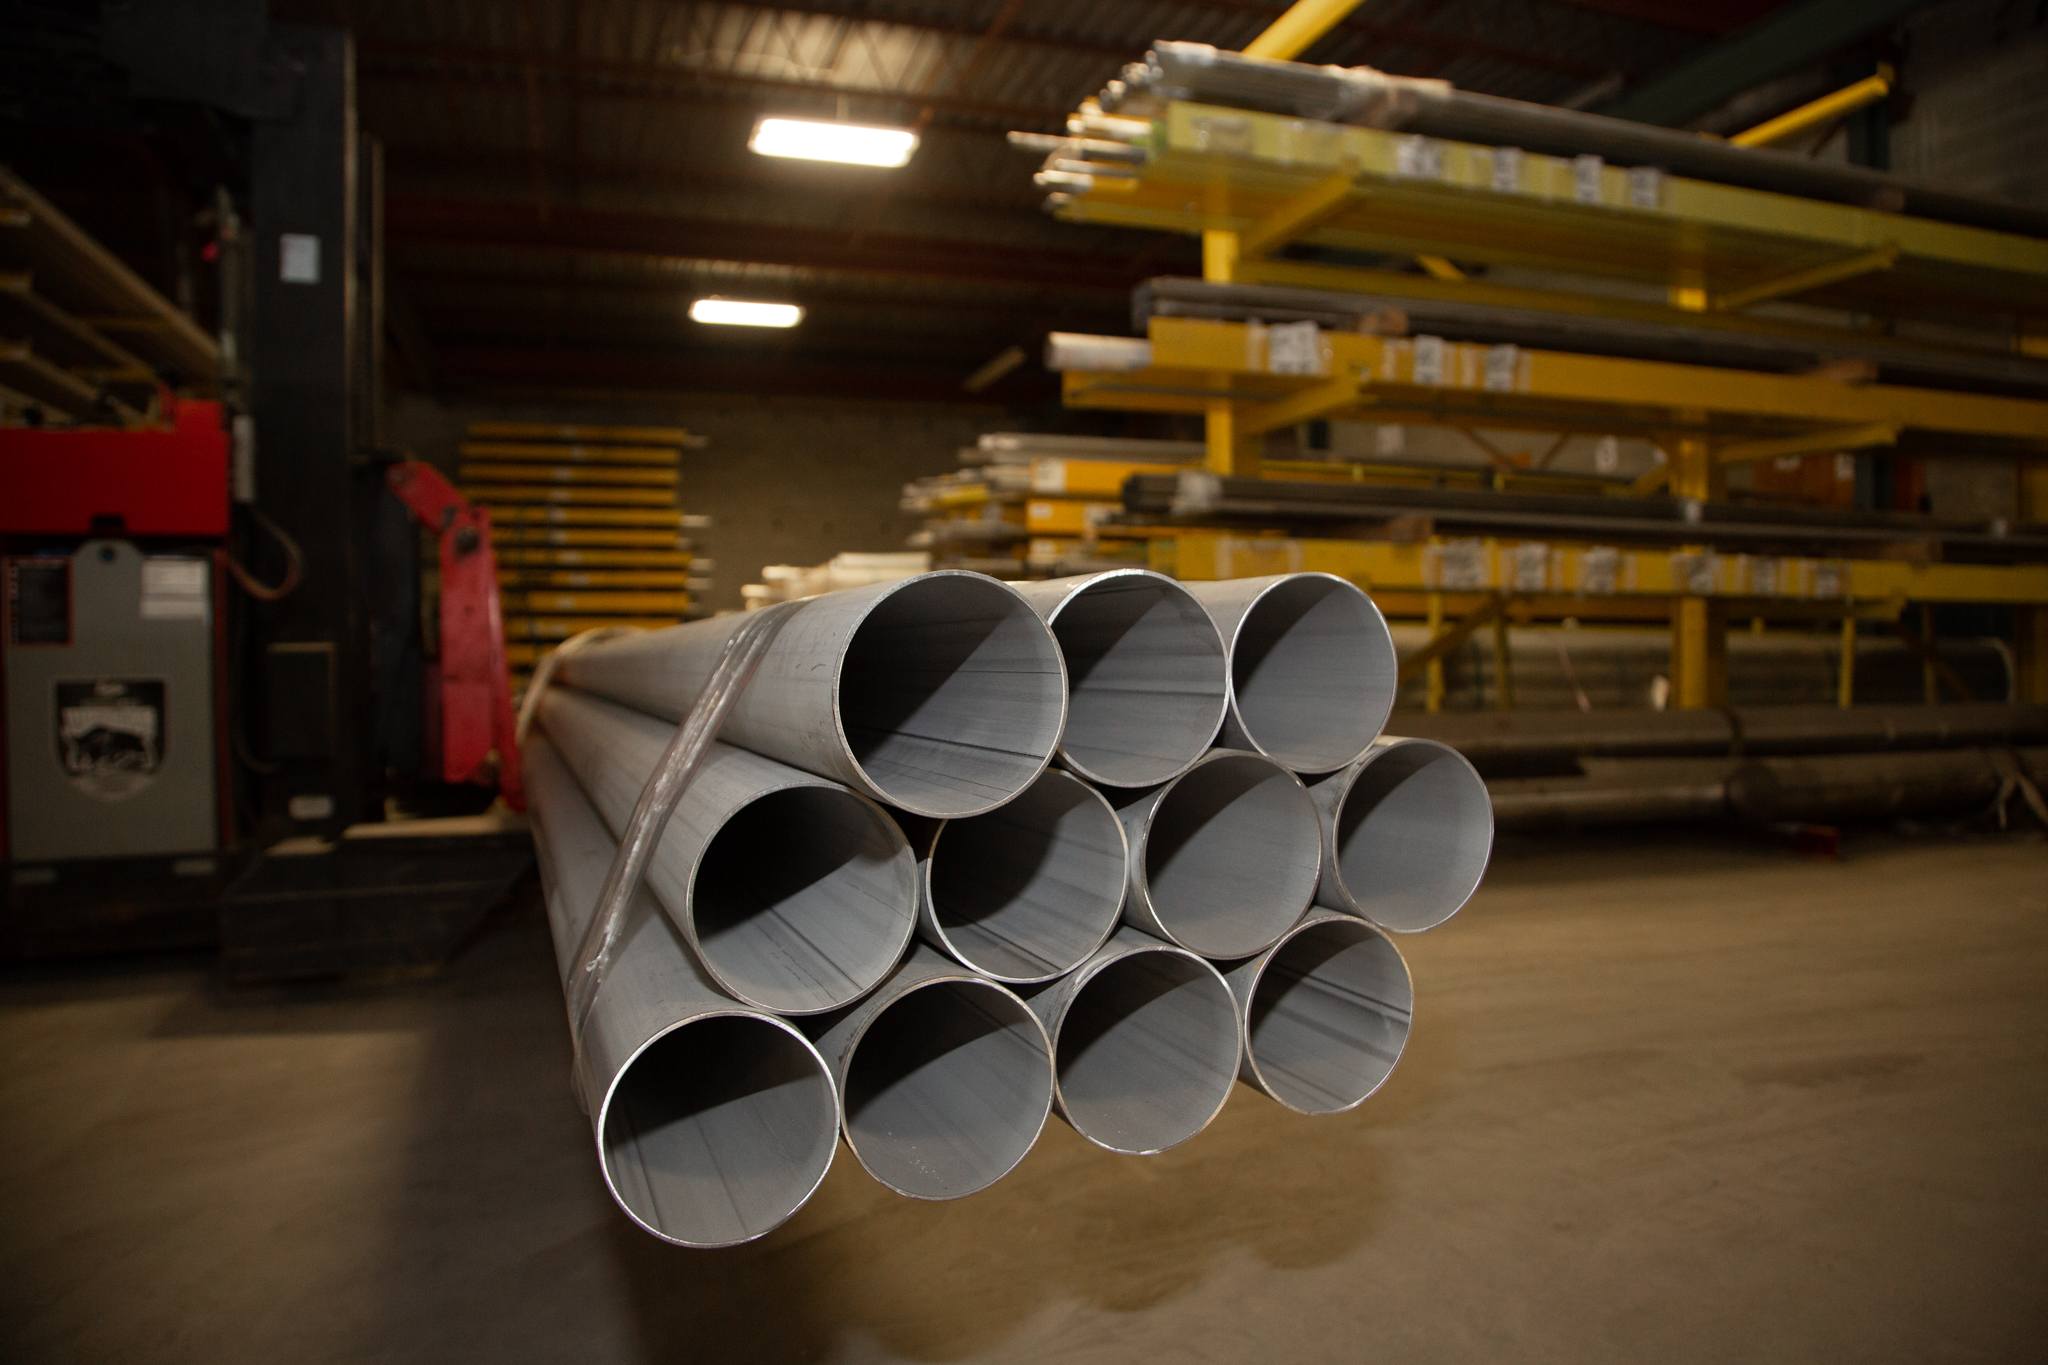
Two routes produce the pipe most industrial buyers specify, and the distinction affects both price and code compliance. Seamless pipe starts as a solid billet, pierced and rolled over a mandrel — no weld seam anywhere in the wall, which is why it’s typically required for high-pressure and high-temperature service under codes like ASME B31.3. Welded pipe is roll-formed from strip and joined with a longitudinal weld, usually more economical and entirely suitable at lower pressures. Both are covered by ASTM A312 for austenitic grades.
The five families of stainless steel
Grades are grouped by crystal structure, which determines how they behave more than the grade number does:
Austenitic — the 300 series
Chromium plus nickel. Non-magnetic, highly formable, excellent weldability, and the broadest corrosion resistance. Around 70% of all stainless produced.
- Common grades: 304, 304L, 316, 316L, 321, 347
- Typical use: process piping, tanks, fittings, food and pharmaceutical equipment
Ferritic — the 400 series
Chromium with little or no nickel. Magnetic, lower cost, good resistance to stress corrosion cracking, but less formable and harder to weld in thick sections.
- Common grades: 430, 409, 439
- Typical use: automotive exhaust, appliance panels, architectural trim
Martensitic
Higher carbon, heat-treatable to high hardness and strength, with corrosion resistance traded away for it.
- Common grades: 410, 420, 440C
- Typical use: valve components, pump shafts, cutlery, wear parts
Duplex
Roughly half austenite, half ferrite. Around twice the yield strength of standard austenitic grades with markedly better chloride stress-corrosion resistance, at lower nickel content.
- Common grades: 2205, 2507 (super duplex)
- Typical use: offshore, desalination, chemical processing, seawater systems
A fifth family, precipitation-hardening grades such as 17-4 PH, combines high strength with moderate corrosion resistance for aerospace and shafting applications. When conditions exceed what any stainless can handle — high-temperature service or aggressive acids — the next step up is nickel and exotic alloys.
304 vs 316: the comparison that matters most
These two austenitic grades account for the majority of stainless sold, and the difference between them comes down to one element.
| Element | 304 / 304L | 316 / 316L |
|---|---|---|
| Chromium | 18.0–20.0% | 16.0–18.0% |
| Nickel | 8.0–10.5% | 10.0–14.0% |
| Molybdenum | — | 2.0–3.0% |
| Carbon | ≤0.08% (L: ≤0.03%) | ≤0.08% (L: ≤0.03%) |
| Manganese | ≤2.0% | ≤2.0% |
| Iron | Balance | Balance |
Composition ranges per ASTM A240. That 2–3% molybdenum in 316 is what buys its chloride resistance — molybdenum stabilises the passive layer specifically against pitting and crevice attack, the failure modes that saltwater, de-icing salts and chloride-bearing process streams cause.
| Consideration | 304 | 316 |
|---|---|---|
| Chloride resistance | Moderate | High |
| Relative cost | Baseline | 10–40% higher |
| Availability | Widest of any grade | Broadly stocked |
| Strength | Comparable | Comparable |
| Best suited to | General industrial, water, food, architectural | Marine, chemical, pharmaceutical, coastal |
Forms, standards and what to specify
Mill product arrives in a handful of standard forms, each governed by its own specification. Knowing which one applies makes your RFQ far easier to quote accurately:
| Form | Governing standard | Specify |
|---|---|---|
| Pipe | ASTM A312 | NPS, schedule, seamless or welded, grade |
| Tube | ASTM A213 / A269 | OD, wall thickness, grade |
| Plate & sheet | ASTM A240 | Thickness, size, finish (2B, No. 4) |
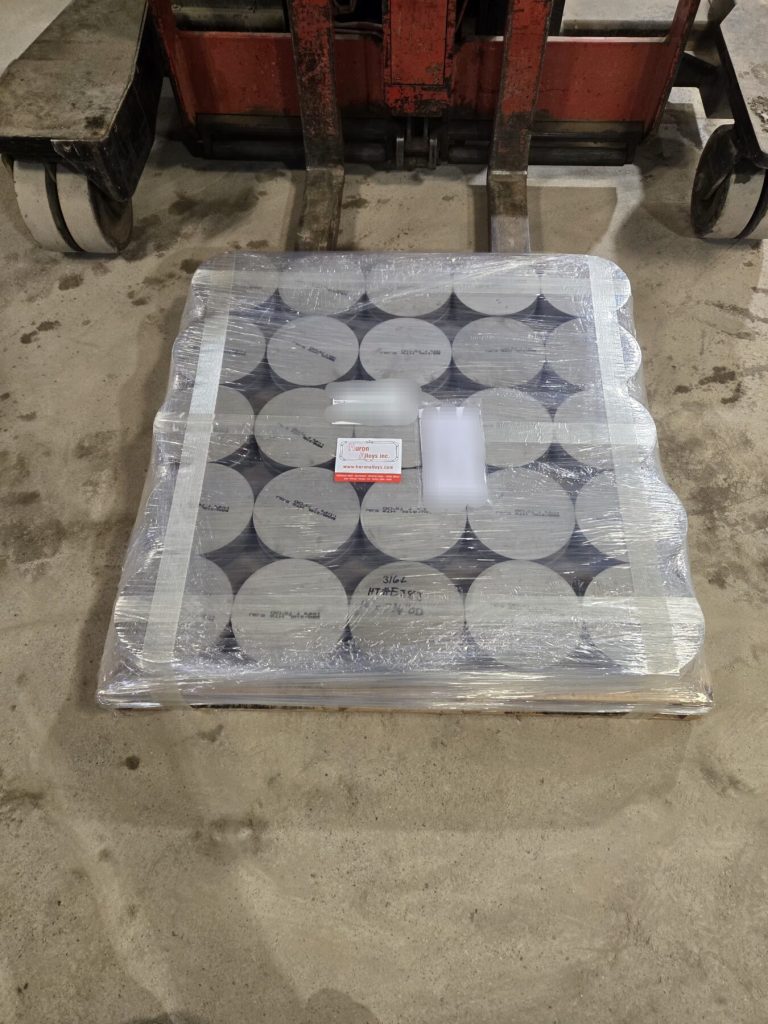
| Bar | ASTM A276 / A479 | Shape, dimensions, condition |
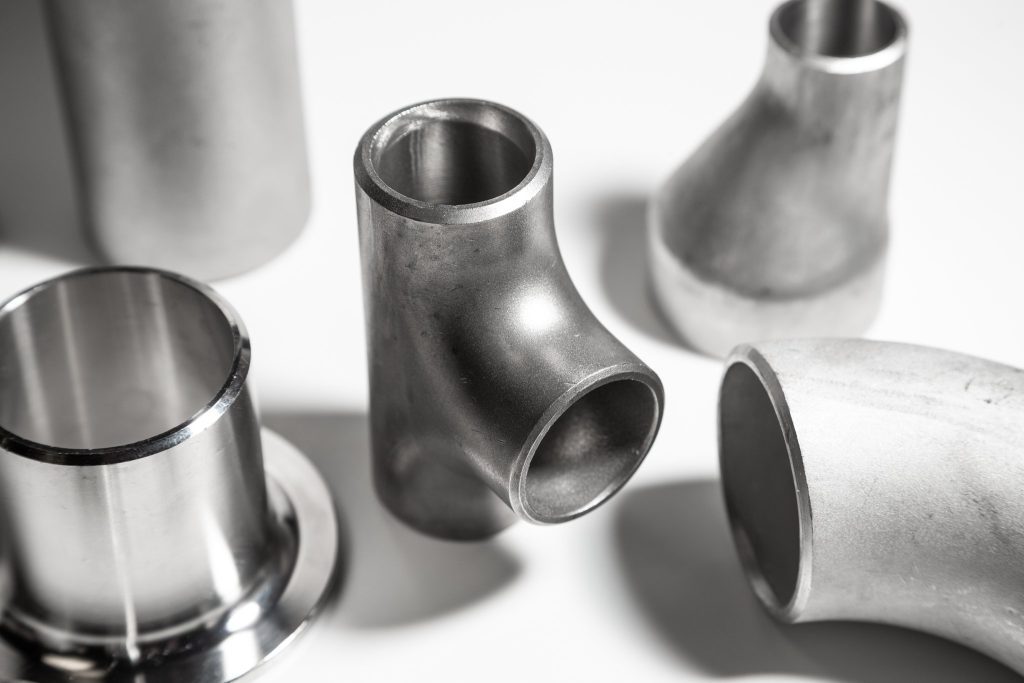
| Butt-weld fittings | ASTM A403 | Size, schedule, fitting type |
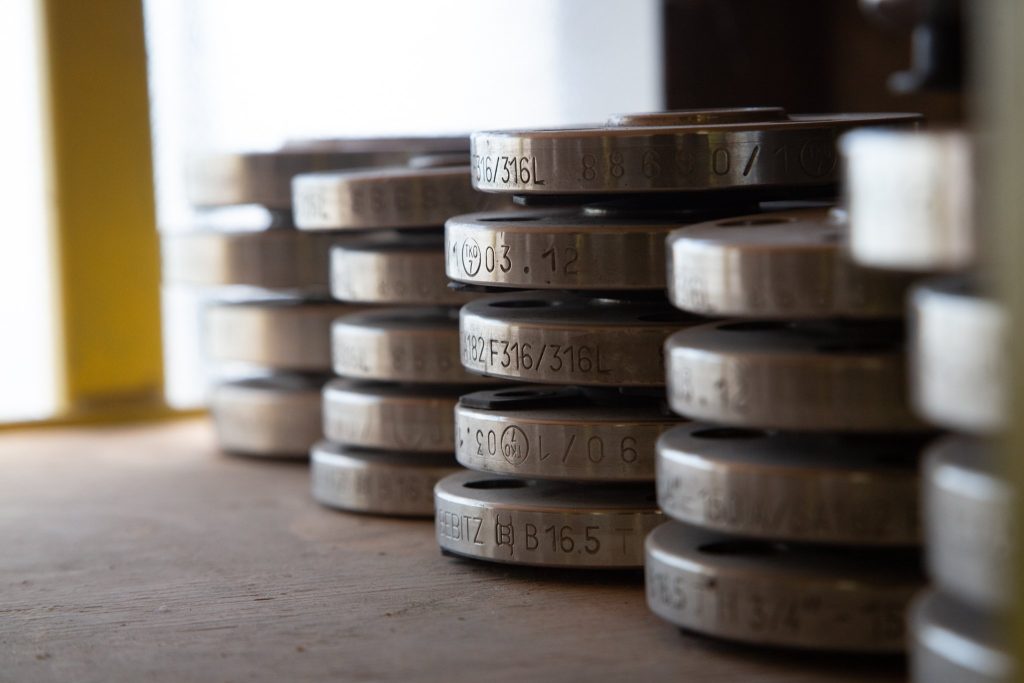
| Flanges | ASTM A182 | Size, class, face type |
Whatever the form, ask for Mill Test Reports with the shipment. An MTR documents chemical composition, mechanical properties, heat number and the applicable specification for the exact heat you received — it’s the only way to prove the material in your hands is what your drawing called for. Our guide to choosing a stainless steel pipe supplier covers what a complete MTR should contain and the documentation red flags worth watching for.
Material rarely ships in the size you need. Plate cut to profile, pipe cut to length, plate bevelled for welding — processing before delivery removes handling and scrap from your shop floor. High-definition plasma handles thick stainless plate quickly and economically, while waterjet cutting produces intricate profiles with no heat-affected zone at all — the right choice for tight tolerances or thermally sensitive parts.
Why it matters
Stainless steel earns its cost over service life rather than at purchase. It needs no coating, tolerates cleaning and sterilisation, holds strength across a wide temperature range, and is fully recyclable at end of life. In a plant where a failed spool means unplanned downtime, the difference between the right grade and a marginal one is measured in production hours, not dollars per kilogram.
- 10.5% chromium minimumIt forms the self-healing passive layer that defines stainless.
- Made from scrapEAF melting, AOD decarburisation, casting, rolling, annealing, finishing.
- Molybdenum is the 304/316 difference2–3% is what buys chloride resistance.
- L grades exist for weldingLow carbon prevents sensitisation at the weld.
- Always take the MTRHeat-level traceability is your only proof of what arrived.
Frequently asked questions
Huron Alloys has supplied stainless steel to Canadian industry since 1983 — 304 and 316 pipe, fittings, flanges, plate, sheet, bar and tube from stock, with plasma and waterjet cutting in-house and MTRs on every order. Tell us what you’re specifying and we’ll confirm availability and pricing.
Specifications cited in this guide. Always consult the current edition for design and compliance.
- ASTM A240/A240M. Standard Specification for Chromium and Chromium-Nickel Stainless Steel Plate, Sheet, and Strip for Pressure Vessels and for General Applications. ASTM International.
- ASTM A312/A312M. Standard Specification for Seamless, Welded, and Heavily Cold Worked Austenitic Stainless Steel Pipes. ASTM International.
- ASTM A276/A276M. Standard Specification for Stainless Steel Bars and Shapes. ASTM International.
- ASTM A403/A403M. Standard Specification for Wrought Austenitic Stainless Steel Piping Fittings. ASTM International.
- ASTM A182/A182M. Standard Specification for Forged or Rolled Alloy and Stainless Steel Pipe Flanges, Forged Fittings, and Valves and Parts for High-Temperature Service. ASTM International.
- EN 10088-1. Stainless steels — List of stainless steels. European Committee for Standardization.
- ASME B31.3. Process Piping. The American Society of Mechanical Engineers.
Reference list current as of publication. Standards are subject to revision — verify the latest editions for critical applications.